Chemical pumps are an essential component in a wide range of industries. They are able to provide an efficient and safe mixing process and dispensing chemical. They are specially designed to handle corrosive and abrasive liquids, that aren’t compatible with standard pumps. Chemical pumps can be classified in two broad categories: centrifugal and positive displacement pumps.
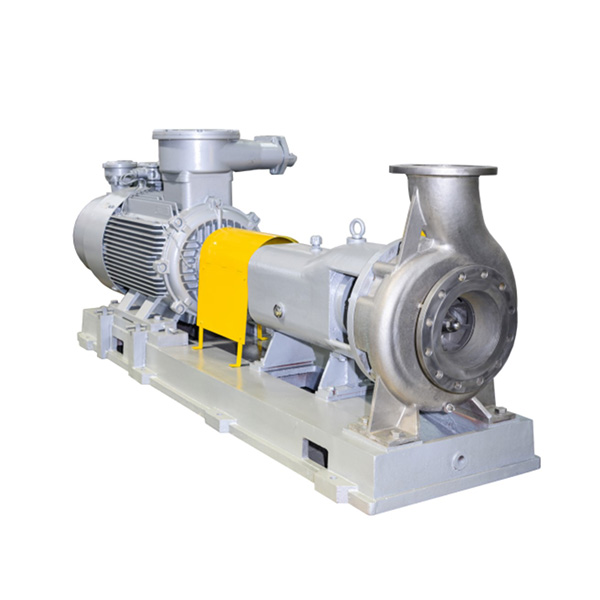
A partnership with reputable chemical pumps manufacturers will ensure access to top-quality pumps that conform to stringent industry standards. These companies make use of their expertise to create chemical pumps that are reliable and durable, as well as efficient and economical. To withstand chemicals that are corrosive or abrasive they make use of advanced technologies in manufacturing, materials, and other methods. By working with trusted manufacturers, businesses can access pumps that are designed to withstand harsh conditions and perform efficiently.
Chemical transfer pump companies specialize in developing pumps specially designed for fluid transfer applications. These pumps can handle a variety chemicals such as acetic and sulphuric acids, sodium hypochlorite and others. Chemical transfer pump manufacturers focus on efficiency in handling fluids They design pumps that have features like corrosion-resistant materials and leak-proof sealings. They also include precise flow control systems. Their pumps are made to ensure safe, precise, and efficient chemical transfer.
Chemical pump suppliers have a vital role to play in connecting businesses to the appropriate pumps to meet their specific requirements. They have a wide assortment of chemical pump options from trusted manufacturers. They have comprehensive product catalogs, technical expertise and support for customers to assist businesses in selecting the right pumps for their requirements. Chemical pumps are available from a variety of options so that companies can select the right pump for their particular industry.
The significance of having chemical pumps that are reliable goes far beyond the protection of fluids. They are crucial for maintaining the integrity and safety of the entire industrial process. An unreliable or malfunctioning pump can lead to expensive leaks, inefficient operation and even potential dangers. When chemicals are involved like chemical manufacturing or petrochemical industry, the consequences of the failure of a pump can be catastrophic. For more information, click chemical pump manufacturers
When investing in dependable chemical pumps, businesses can minimize the risks of handling fluids. These pumps are designed and built to withstand the corrosive properties of various chemicals, which means they operate reliably and efficiently over time. The pumps are built with strong materials and the most advanced sealing mechanisms. They also have precise flow control.
In addition, dependable chemical pumps usually come with complete maintenance and support. The manufacturers and suppliers recognize the significance of these pumps, so they offer technical assistance in the form of spare parts, as well as routine maintenance tests. This proactive approach allows you to identify and resolve any problems before they become serious which ensures that the pump is always reliable and minimizing any unplanned downtime.
Chemical pumps have applications in various industries, including chemical manufacturing, petrochemicals and food processing. They serve as vital components for fluid flow, mixing and dispensing. Chemical pumps are also employed in high-temperature heating systems and for off-site use in refineries. Chemical pumps are a must-have tool for industrial processes due their ability to work with challenging fluids.
It is essential to take into account factors like the kind of fluid being used as well as the flow requirements, operating conditions, and compatibility. The most reliable suppliers and manufacturers provide assistance and guidance in selecting the right pump for your specific needs. When deciding on a pump it is vital to take into consideration the safety, reliability, and effectiveness to reduce the risk of accidents while also maximizing productivity. ensure that there is no downtime.
Chemical pumps can be used for applications that extend far beyond the refinery. These pumps are versatile and play an essential role in transferring chemicals from the site. Chemical pumps are crucial for efficient refinery operations, whether they’re used to transport liquids that are corrosive into storage, facilitate the loading and unloading tanker trucks as well as support maintenance and repair or to ensure that corrosive chemicals can be transported. The durability, reliability and unique features of these pumps make them vital tools for off-site applications, where the handling of chemical substances that are corrosive or abrasive requires precision, efficiency, as well as safety. By investing in top-quality chemical pumps and working with reliable manufacturers and suppliers, refineries can maintain the foundation of their operations off-site and have flawless and efficient chemical transfer in a variety of settings.